How to Choose an Electronic Board Assembly Supplier in 2026

Choosing an electronic board assembly supplier in 2026 means looking beyond a polished quote. A low unit price can hide setup costs, long lead times, or fragile processes. The real test is whether a supplier can build your design consistently, explain its controls, and respond when something goes wrong.

Quality pioneer W. Edwards Deming is often associated with the principle, “Quality is everyone’s responsibility.” That idea matters on an assembly line. A reliable partner connects engineering, purchasing, production, and inspection instead of treating quality as a final checkpoint. Ask how the team handles component traceability, solder-paste control, inspection findings, and engineering changes. Request examples, not just assurances. A clear process beats a confident pitch.

Small details matter. A supplier’s answers about first-article approval, test coverage, and nonconforming boards can reveal how work actually moves through the factory. Look for relevant experience with your board complexity and volume, plus capacity that fits your schedule. Review documentation and references where available. A neat audit file can still miss a weak handoff, so conversations with the people who manage production are useful too. No checklist catches everything.

This guide examines practical ways to compare suppliers, assess quality systems, and spot trade-offs before committing. It also considers communication, scalability, and total cost—not only the number on the quote. The best choice may not be the largest factory or the cheapest one. It is the partner whose capabilities match your product, whose evidence supports its claims, and whose limitations are discussed openly.
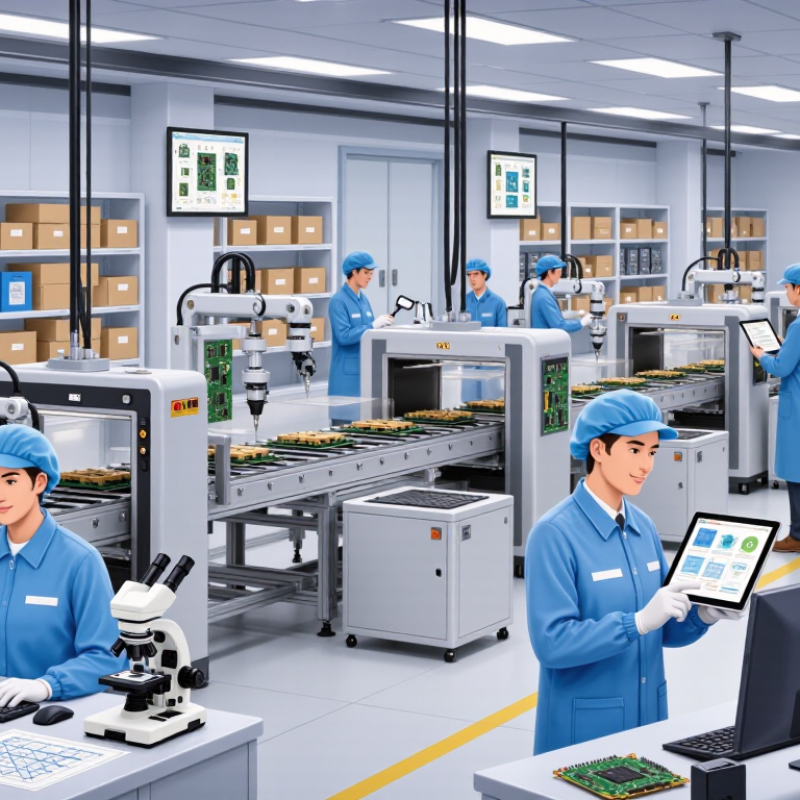
How to Choose an Electronic Board Assembly Supplier in 2026

Define the Board Assembly Requirements and Project Constraints

Before comparing suppliers, translate product use into measurable assembly requirements. Define board dimensions, layer count, base material, copper weight, component package sizes, and expected production volume. Specify whether the project needs prototypes, a pilot run, or recurring builds. Small details matter. A fine-pitch processor and a tall connector can require different placement and inspection capabilities. Include operating conditions such as vibration, humidity, and temperature range.

Set acceptance criteria before requesting quotes. Describe soldering standards, inspection methods, test coverage, labeling, and packaging needs. Provide current design files, a controlled bill of materials, and clear notes for parts with approved alternatives. If a functional test fixture is required, state who will supply it and when. Ambiguity costs time. Even a missing polarity mark can trigger questions or rework.

Then document the project constraints: target cost, delivery window, forecast changes, and minimum order expectations. Separate firm limits from preferences; a fixed launch date is not the same as a hoped-for price. Ask suppliers to identify assumptions, long-lead components, and risks in writing. Requirements often change after the first prototype, and that is normal. Still, changing files without tracking revisions can create avoidable confusion. Review the specification with engineering and purchasing before sending it out.
How to Choose an Electronic Board Assembly Supplier in 2026: Define Requirements and Project Constraints

Use this illustrative timeline to discuss schedule constraints with potential suppliers. The planning allowances are examples, not industry benchmarks; actual lead times depend on board complexity, component availability, order quantity, and testing scope. Confirm each estimate against your project requirements.

Assess Supplier Capabilities, Equipment, and Engineering Support

A capable electronic board assembly supplier should match its process to your product, not just quote a low unit price. Ask which board types and component packages it handles regularly, and request examples of similar production runs. Details matter. A line built for high-volume standard boards may struggle with frequent changeovers or fine-pitch components.

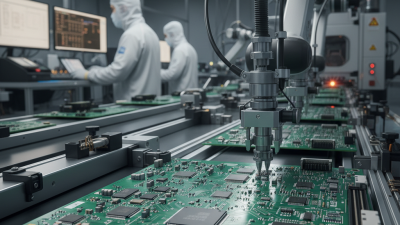
Look beyond an equipment list. Ask how the supplier controls solder paste, verifies placement, and manages reflow profiles. Automated optical inspection can catch visible defects; X-ray inspection may help with hidden solder joints. Ask how inspection results are recorded and linked to each production lot. A machine’s presence is not proof of a reliable process. Request sample reports or a walkthrough of the actual workflow.

Engineering support matters before the first production run. A useful team can review board files, flag component spacing or panelization concerns, and discuss test access early. Ask who handles questions when a part is unavailable or a design revision arrives mid-build. A polished capability sheet can still hide a weak handoff. I would not reject a supplier over every missing machine, though; some steps can be handled through qualified partners. Confirm how those handoffs are controlled, and who owns the outcome.

Evaluate Quality Systems, Certifications, and Regulatory Compliance

An assembly supplier’s certificate is only a starting point. Ask for its scope, covered facility, expiry date, and recent audit findings. ISO 9001 certification alone does not prove that every production line follows the same controls. Check whether the site applies IPC J-STD-001 and IPC-A-610 criteria where appropriate. For medical or automotive boards, verify that ISO 13485 or IATF 16949 certification covers the actual facility and work involved. Scope matters more than logos. Request redacted evidence of corrective actions, calibration records, and operator training, not just a certificate wall.

Regulatory controls should be traceable to the board and its materials. Ask how the supplier checks applicable RoHS and REACH requirements, maintains material declarations, and flags changes in components or processes. Can it trace a finished board back to its component lots, inspection results, and rework history? Ask to see a sample record. Deloitte’s 2024 Smart Manufacturing Survey found that 86% of surveyed manufacturing executives expected smart manufacturing solutions to drive competitiveness within five years. That makes digital records worth checking, though software alone cannot guarantee accuracy. No system is perfect. Review how staff catch missing data, contain nonconforming boards, and verify corrective actions actually work.

Review Supply Chain Resilience, Lead Times, and Cost Structure

Choosing an electronic board assembly supplier in 2026 means looking beyond the quoted unit price. Ask how the supplier handles a delayed microcontroller, a sudden allocation change, or a shipment held at a regional hub. Request a sample risk review naming alternate components, approval steps, and update responsibilities. Ask for evidence. A polished dashboard is useful, but it cannot replace a clear escalation path.

Lead time needs a precise definition. Does the quoted schedule begin after order placement, approved files, or component arrival? Compare standard and expedited builds, then check on-time delivery records for boards of similar complexity. A supplier should separate queue time, fabrication, assembly, inspection, and shipping. Confirm how often status updates arrive when a part slips. Forecasts can be wrong; the response matters more than false certainty.

Scrutinize the cost structure, too. Separate tooling, setup, programming, inspection, packaging, freight, and recurring unit costs. Ask which prices depend on volume and which may shift with component availability. Review payment milestones and engineering-change costs before production. Keep a modest buffer for yield loss or urgent freight, but ask what triggers those charges. This is easy to overlook. I would not choose solely by the lowest quote, though a higher price does not prove resilience. Compare documented capacity, response times, and cost assumptions against your demand plan.

Validate Shortlisted Suppliers Through Audits and Pilot Builds

How to Choose an Electronic Board Assembly Supplier in 2026

A supplier audit should test the process, not the presentation. Ask to trace one board from incoming components to shipment. Check lot records, moisture-sensitive device storage, solder-paste controls, reflow profiles, and inspection results. Verify that operators follow documented work instructions at the line. A polished factory tour proves little on its own.

Tips: Bring a sample bill of materials and a known defect scenario. Ask how the supplier would contain affected boards, identify the lot, and report the cause. Check that corrective actions have owners and due dates.

Then run a pilot build using your actual design and approved materials. Record first-pass yield, defects by type, rework time, and delivery performance. Compare results with agreed acceptance criteria, including IPC workmanship requirements where applicable. Deloitte and MAPI’s 2024 Smart Manufacturing Survey found that 86% of manufacturing executives expect smart manufacturing to drive competitiveness within five years. That makes it worth checking whether a supplier can show usable production data, not just promise digital visibility. A pilot is still a small sample; it cannot guarantee stable volume production. Ask what changes between pilot and full-rate builds, and how each change is controlled. One detail is easy to miss: confirm who owns test fixtures and process records after the trial ends.

How to Choose an Electronic Board Assembly Supplier in 2026 - Validate Shortlisted Suppliers Through Audits and Pilot Builds

Evaluation dimension What to verify in the audit What to measure in the pilot build Practical decision guidance
Quality management system Review the current quality certificate and its scope, internal audit records, corrective-action process, document control, and management of nonconforming product. ISO 9001 is a general quality-management standard; sector-specific requirements may also apply. Check that the approved build documents, inspection records, deviations, and corrective actions are complete and traceable to the pilot lot. Confirm that the certified scope covers the relevant site and activities. Agree on applicable customer and regulatory requirements before awarding production work.
Process and workmanship controls Observe solder-paste printing, component placement, reflow or wave soldering, inspection, and rework controls. Review process instructions, equipment maintenance, operator training, and control of process changes. Review inspection results and defects by type and process step. Confirm workmanship criteria are defined in the purchase documents; IPC-A-610 and J-STD-001 are commonly used industry standards when specified by agreement. Require the supplier to identify the exact standard, revision, and acceptance class agreed for the product. Do not assume a class or workmanship standard applies unless documented.
ESD and handling Check the ESD control program, protected areas, grounding checks, packaging, staff training, and records. ANSI/ESD S20.20 is a recognized standard for developing an ESD control program. Inspect handling and packaging from assembly through shipment. Verify that ESD-sensitive assemblies and components are identified and protected as specified. Look for documented controls and evidence they are followed in the actual production area, rather than relying on a policy document alone.
Component sourcing and traceability Review approved sourcing channels, incoming inspection, counterfeit-risk controls, material-status controls, and procedures for customer-supplied parts and substitutions. Trace selected components from the pilot assembly back to purchase and receiving records, including lot or date-code information where available. Check that substitutions were authorized. Set traceability requirements by component and product risk. Require prior written approval for any bill-of-material or manufacturer-part change.
Inspection and test coverage Review how inspection methods are selected and maintained. Determine whether solder-paste inspection (SPI), automated optical inspection (AOI), X-ray inspection, and electrical or functional testing are available and appropriate to the design. Compare the test plan with product risks and design requirements. Review actual inspection and test records, including coverage limits, failed units, retests, and disposition. Match methods to the assembly: for example, X-ray may help inspect hidden solder joints, while functional testing checks specified operating behavior. No single method replaces a complete, agreed test plan.
Pilot yield and defect management Check how the supplier defines first-pass yield, records defects, performs root-cause analysis, and verifies corrective actions. Confirm yield data can be tied to a specific product, process, and lot. Record units entering the agreed test stage, units passing without repair or retest, defect categories, rework, scrap, and retest results. Calculate first-pass yield consistently as first-pass units divided by units tested. Agree on sample size and acceptance criteria before the build. Treat pilot results as product- and process-specific evidence; do not compare percentages without checking the calculation and test scope.
Engineering readiness and change control Assess design-for-manufacturing feedback, engineering escalation routes, revision control, deviation approval, and notification of process or material changes. Check whether build issues—such as unclear drawings, footprint concerns, or test-access limitations—were raised, documented, and resolved through approved changes. Use controlled, released files for the pilot. Document all approved deviations and ensure the final build package reflects the agreed revision.
Capacity and production planning Review relevant equipment, staffing, maintenance, scheduling practices, bottlenecks, and contingency plans for material or equipment disruptions. Compare the pilot schedule with actual material readiness, build time, inspection and test time, and shipment date. Record constraints that could affect the proposed production volume. Request a capacity plan for the expected mix and volume. Validate claims against the equipment and resources available at the audited site.
Packaging and delivery condition Review packing instructions, product protection, labeling, shipment records, and controls for moisture-sensitive devices where applicable. Inspect pilot packaging and labels against the agreed requirements. Check that handling and storage instructions accompany the shipment when required. Define packaging, labeling, and delivery requirements in the order documents, including any product-specific moisture-sensitivity controls.
Final qualification decision Document audit findings, evidence reviewed, open corrective actions, owners, and due dates. Distinguish critical gaps from lower-risk improvement items. Review the completed build report, inspection and test evidence, defect disposition, traceability records, and any unresolved technical issues. Approve, conditionally approve, or defer qualification using criteria agreed in advance. Close critical gaps and confirm corrective-action effectiveness before scaling production.

Note: Acceptance criteria, sample size, applicable standards, and required records should be agreed between the buyer and supplier for the specific product and market.